


BAER TriTap Set HSSE-VAP: Tap blind hole | Core drill: M 3 - 12
In stock


Express shipping available
BAER TriTap Set HSSE-VAP: Tap blind hole | Core drill: M 3 - 12
This TriTap thread tap set for blind holes is a high-quality and versatile set for all requirements in precise thread cutting in blind holes. It includes machine taps in sizes M3 to M12 as well as matching twist drills with three-flat shanks for accurate core hole drilling. What makes TriTap special: In addition to the square shank, the taps also feature a three-flat shank, ensuring a secure grip even in handheld machines. This allows the tools to be used both in stationary machines such as CNC systems and thread cutting machines, as well as flexibly in hand-held drills.
Manufactured from high-alloyed HSSE steel with 5% cobalt and a vaporized surface, the TriTap taps offer extreme wear resistance, high heat resistance, and a long service life. The special geometry of the blind hole version ensures controlled chip evacuation upward from the blind hole, reduces the risk of chip accumulation, and enables a precise, dimensionally accurate thread to the bottom of the bore. This makes the set suitable even for difficult-to-machine materials such as stainless steel. The TriTap blind hole thread tap set comes in a robust plastic box that ensures safe transport and organized storage. A set no workshop should be without.
Tip for optimal results: Always start thread cutting at a low speed to allow the first threads to cleanly engage with the workpiece. This ensures smooth and precise results from the beginning. Also make sure to guide the tap straight and perpendicular to the bore. This ensures even load distribution and consistently perfect results – even with demanding materials.
Dimensions
| Diameter |
3 - 12 |
|---|---|
| Dimension |
M 3 - 12 |
Characteristics
| Product group |
threading tool sets |
|---|---|
| Product type |
Threading tool sets |
| Thread standard |
M: Metric ISO standard thread according to DIN 13 |
| Tolerance |
ISO2/6H |
| Direction |
Right |
| Tensile strength at room temperature |
up to 1200 N/mm² | 38 HRC |
| Material |
HSSE VAP |
Technical information – Screw taps

Blind hole up to 2.5 x D

Form C 35° RSP

2-3 threads

see illustration

External cooling and lubrication

HSSE VAP

up to 1200 N/mm² | 38 HRC

ISO2/6H
Set content
| BAER UNiTap HSSE machine tap for blind hole | M 3 x 0,5 | M 4 x 0,7 | M 5 x 0,8 M 6 x 1,0 | M 8 x 1,25 | M 10 x 1,5 M 12 x 1,75 |
|---|---|
| BAER HSSE core drill bits | 2,5 mm | 3,3 mm | 4,2 mm | 5,0 mm 6,8 mm | 8,5 mm | 10,2 mm |
Applications
- Steels and steel alloys up to 1200 N/mm²
- Stainless steels up to 1000 N/mm²; stainless steels; stainless steels; VA steels, INOX, V2A, V4A
- Lamellar graphite cast iron (GG) and with spheroidal graphite (GGG) up to 1000 N/mm²; grey cast iron, nodular graphite cast iron
- Pure titanium and titanium alloys up to 900 N/mm²
- Pure nickel and nickel alloys up to 900 N/mm²
- All cast and wrought aluminium alloys
- Copper, copper alloys and brass (all chip lengths)
- for manual and machine use
Application – Sample materials for taps
| Soft magnetic iron, construction steels, free-cutting steels, case-hardening steels | Cutting speed vc in m/min | |
|---|---|---|
| 1.1014 | RFe80 | 25 - 50 |
| 1.0570 | St52-3 | 25 - 50 |
| 1.0718 | 9SMnPb28 | 25 - 50 |
| 1.6523 | 20NiCrMo2 | 6 - 30 |
| Carbon steel, spring steel, alloyed steel, quenched and tempered steel | Cutting speed vc in m/min | |
|---|---|---|
| 1.0503 | C45 | 20 - 30 |
| 1.1269 | Ck85 | 20 - 30 |
| 1.7218 | 25CrMo4 | 6 - 30 |
| 1.2344 | X40CrMoV5-1 | 6 - 30 |
| Stainless steels (ferritic, austenitic, martensitic) | Cutting speed vc in m/min | |
|---|---|---|
| 1.4104 | X14CrMoS17 | 12 - 35 |
| 1.4301 | X5CrNi18-10 (V2A) | 12 - 15 |
| 1.4571 | X6CrNiMoTi17-12-2 (V4A) | 12 - 15 |
| 1.4125 | X105CrMo17 | 12 - 15 |
| Grey cast iron | Cutting speed vc in m/min | |
|---|---|---|
| 0.6010 | GG10 | 35 - 50 |
| 0.6020 | GG20 | 35 - 50 |
| 0.6030 | GG30 | 35 - 50 |
| 0.6040 | GG40 | 35 - 50 |
| Spheroidal graphite cast iron, malleable cast iron | Cutting speed vc in m/min | |
|---|---|---|
| 0.7040 | GGG40 | 12 - 45 |
| 0.7060 | GGG60 | 12 - 45 |
| 0.7070 | GGG70 | 12 - 45 |
| 0.8035 | GTW35-04 | 10 - 25 |
| Pure titanium and titanium alloys | Cutting speed vc in m/min | |
|---|---|---|
| 3.7024 | Ti99.5 | 3 - 15 |
| 3.7034 | Ti99.7 | 3 - 15 |
| 3.7165 | TiAl6V4 | 1 - 5 |
| 3.7174 | TiAl6V4Sn2 | 1 - 5 |
| Pure nickel and nickel alloys | Cutting speed vc in m/min | |
|---|---|---|
| 1.3926 | RNi12 | 3 - 10 |
| 2.4668 | NiCr19Fe19NbMo (Inconel 718) | 3 - 10 |
| 2.4630 | Ni-Cr20Ti (Nimonic 75) | 1 - 5 |
| 2.4665 | NiCr22Fe18Mo (Hastelloy X) | 1 - 5 |
| Pure copper and copper alloys, brass, bronze (all chip lengths) | Cutting speed vc in m/min | |
|---|---|---|
| 2.0065 | E-Cu 58 | 50 - 60 |
| 2.1247 | CuBe2 | 30 - 65 |
| 2.0360 | CuZn40 | 30 - 65 |
| 2.1020 | CuSn6 | 12 - 20 |
| Pure aluminum, aluminum cast and wrought alloys (all chip lengths) | Cutting speed vc in m/min | |
|---|---|---|
| 3.0205 | Al99 | 50 - 65 |
| 3.1645 | AlCuMgPb | 50 - 65 |
| 3.2373 | G-AlSi9Mg | 40 - 65 |
| 3.2583 | G-AlSi12(Cu) | 40 - 65 |
Cutting speed vc [m/min] = (Outer diameter * π * speed) / 1000
Rotation speed n [1/min] = (Cutting speed in m/min * 1000) / (Outer diameter * π)
Feedrate programming [mm/min] = speed * pitch
Please note that the above cutting speeds are indicative and must be adjusted depending on lubrication and actuation.
Further information
Safety instructions
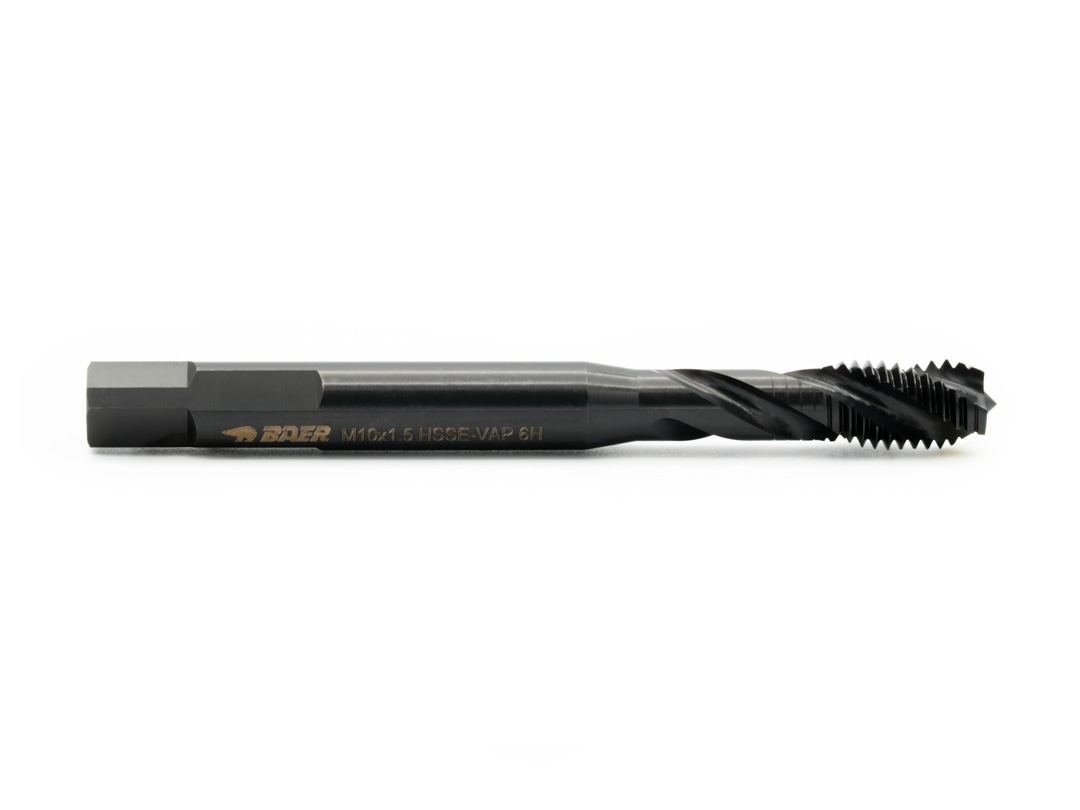
TriTap Blind Hole – Flexibility Meets Precision
The unique shank geometry of the TriTap blind hole taps enables secure use in both machines and handheld tools. The three flat surfaces on the shank ensure a stable and secure grip even in a standard chuck, preventing the tool from slipping. Especially useful for mobile use or when no stationary machine is available. The special blind hole geometry ensures short cutting edges and optimized chip evacuation upwards – ideal when the tap must finish at the bottom of the hole. This allows precise threads to be produced safely, even in blind holes.
Advantages of the TriTap Thread Tap:
- Innovative shank design for secure hold even in handheld machines
- Universal use – even suitable for stainless steel!
- Top quality and long tool life thanks to HSSE-VAP
- Suitable for nearly every application
- Long service life
- Ideal for all workshops and professionals with varying requirements
- Huge cost savings – only one tool needed for all applications
BAER TriTap HSSE-VAP Machine Tap – Form C 40° RSP:
M 3 x 0.5 | M 4 x 0.7 | M 5 x 0.8 | M 6 x 1.0 | M 8 x 1.25 | M 10 x 1.5 | M 12 x 1.75
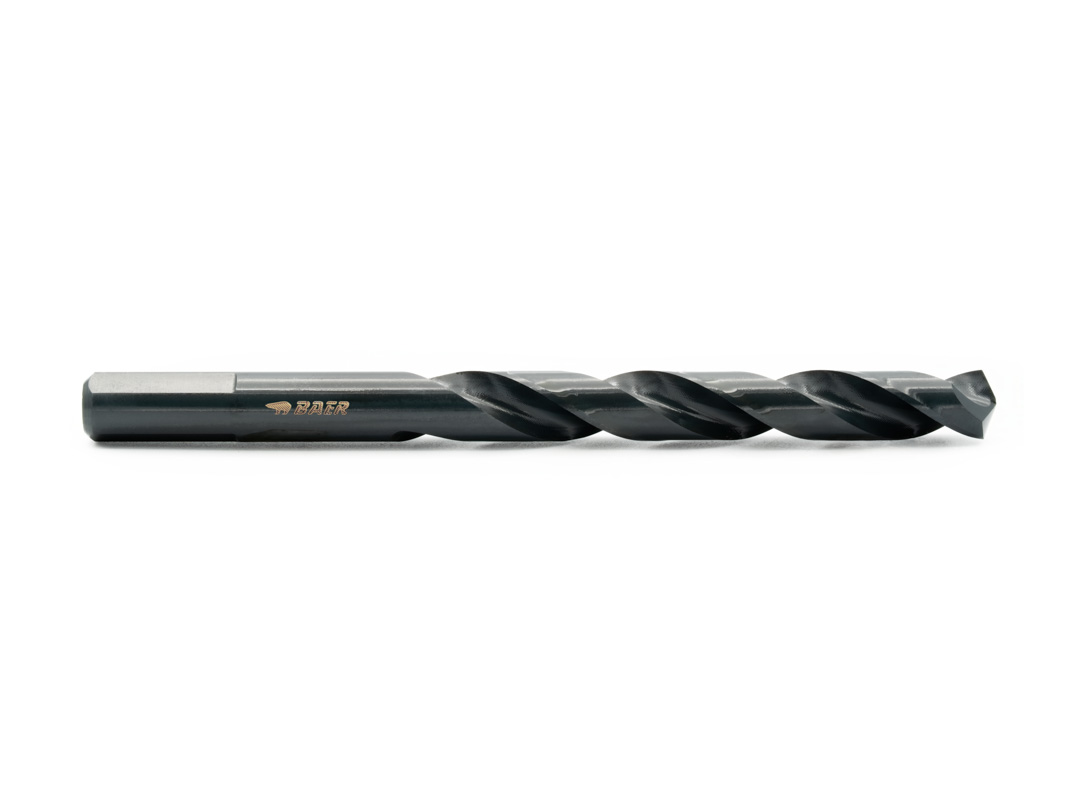
HSSE-VAP Twist Drills with Three-Flat Shank for Core Drilling
#non-negotiable
Almost every DIY enthusiast has used them before: the classic drill bits for cordless screwdrivers, drills, hammer drills, or rotary hammers. The key to proper drill selection is not only the material but also the cutting geometry, chip angle, and helix angle – known as the spiral pitch. These drills are particularly robust, made of high-alloyed HSSE/Cobalt steel with excellent heat resistance and outstanding concentricity. Perfect for drilling in iron, steels, cast materials, bronze, tempered and case-hardened steels up to 1200 N/mm², as well as in high-strength CrNi-based alloys and stainless, acid-resistant, and heat-resistant steels such as V2A, V4A, and INOX. Core hole drilling is essential for subsequent internal thread cutting.
HSSE-VAP Core Hole Drills DIN 338 for M 3 - M 12:
Ø 2.5 mm (M 3) | Ø 3.3 mm (M 4) | Ø 4.2 mm (M 5) | Ø 5.0 mm (M 6) | Ø 6.8 mm (M 8) | Ø 8.5 mm (M 10) | Ø 10.2 mm (M 12)
Login